Petrochemicals are a pillar industry of the national economy, with the entire industrial chain covering oil and gas extraction, refining, chemical synthesis, and oil and gas storage and transportation. The production processes involve various media that are flammable, explosive, highly toxic, corrosive, and easily permeable, while also experiencing extreme coupled conditions such as ultra-high temperature and pressure, cryogenic high vacuum, high solids content, and high-speed rotation. Safety management and sealing requirements are extremely stringent.
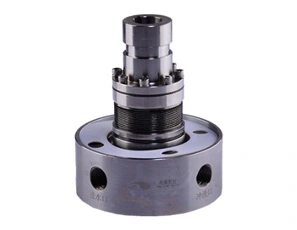
Traditional seals are inherently limited by contact wear, insufficient weather resistance, and poor anti-pollution capabilities, frequently resulting in leakage and failure. This not only leads to high maintenance and downtime losses but also poses significant safety and environmental risks such as combustion, explosion, poisoning, and VOCs exceeding standards. Ferrofluid Seal (Magnetic Fluid Seal), with their core characteristics of non-contact zero wear, absolute zero leakage, wide temperature range resistance, and long lifespan, systematically solve the sealing pain points of the petrochemical industry and are the optimal solution for extreme operating conditions in this field.
Sealing Challenges
1. Media Compatibility and Leakage Safety Risks
The core media contains highly toxic hydrogen sulfide, Class A flammable and explosive light hydrocarbons, and highly corrosive naphthenic acids/sulfides. Traditional sealing materials are prone to swelling, aging, and hydrogen embrittlement cracking. Lightweight small molecules can easily penetrate and cause micro-leaks, directly causing combustion, explosion, poisoning risks, and VOC exceedances.
2. Stability Loss Under Extreme Coupled Operating Conditions
The operating conditions span a wide range, covering scenarios such as downhole ultra-high pressure, ultra-high temperature in hydrogenation units, cryogenic separation of ethylene, high-speed rotating equipment, and large-shaft-diameter eccentric agitators. Traditional seals are prone to thermal deformation, end-face wear, and liquid film instability, leading to sudden failures.
3. The Maintenance Cost Dilemma of Long-Cycle Operations
Mainstream refining and chemical plants adhere to a "four-year turnaround" standard. Unplanned shutdowns can result in losses of millions of yuan per day. Traditional seals have short lifespans, requiring frequent shutdowns for maintenance, causing huge economic losses and high operational safety risks. The associated flushing systems also increase environmental costs.
4. Wear and Clogging Problems under High Solid Content Conditions
The entire process generally contains solid media such as sand, catalyst particles, coke powder, and polymer powder, which can easily cause erosion wear of traditional seals, blockage and jamming of compensation mechanisms, significantly shorten service life, and even cause sudden leaks.
Solutions
1. Dedicated Media-Resistant Material System, Addressing Corrosion and Penetration Risks at Their Root
Customized perfluoropolyether-based magnetic liquid is completely immiscible and non-reactive with acidic and alkaline media, offering corrosion-resistant. Under strong magnetic field confinement, it forms a stable sealing liquid ring.
2. Customized Structure for Extreme Operating Conditions, Stable Adaptability Across All Scenarios
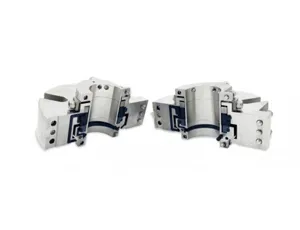
Precisely optimized for wide-range coupling conditions: Double-layer constant-temperature jacket + high-pressure multi-stage pole tooth structure for ultra-high temperature and high-pressure conditions; customized low-freezing-point magnetic liquid for cryogenic conditions, adaptable to extreme high vacuum; optimized magnetic pole structure for high-speed equipment, adaptable to high speeds, with controllable temperature rise; modified split structure, allowing for rapid installation without disassembling core components, significantly shortening downtime.
Non-contact design with no mechanical wear, continuous operating life under normal conditions can reach more than 2 years, fully matching the long-cycle operation requirements of refining and chemical plants, eliminating the need for mid-term shutdowns for maintenance.
① Core Application Scenarios
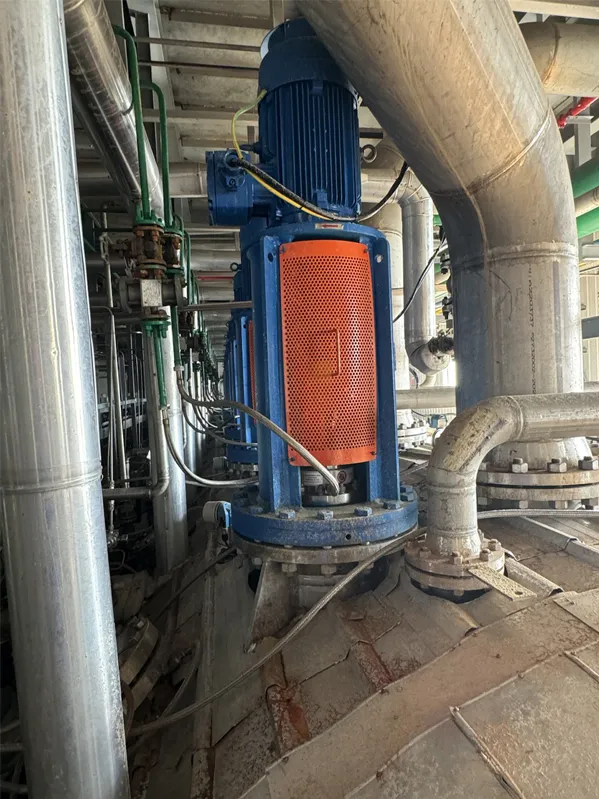
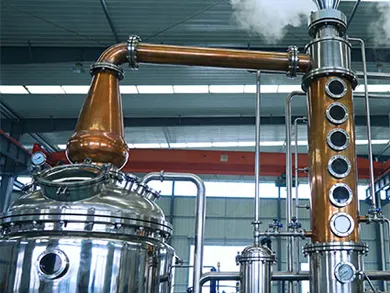
Application Scenarios: Primarily used in core processes such as crude oil atmospheric and vacuum distillation, catalytic cracking, hydrocracking, olefin polymerization, and aromatics production. Core equipment includes reactors, agitators, rotary shafts, centrifugal pumps, compressors, vacuum pumps, flange valves, and tank mixing equipment, among other critical sealing components.
Core Pain Points:
•Complex media, including highly corrosive, flammable, and explosive media such as hydrogen sulfide, chloride ions, strong acids and alkalis, and organic solvents. Traditional sealing materials are prone to corrosion, swelling, aging, and rapid failure.
•Harsh operating conditions, covering a wide temperature range, high vacuum, and high speed, with large pressure and temperature fluctuations. Traditional seals are prone to gap changes, wear, and leakage.
•The equipment requires long-term continuous operation. Traditional seals require frequent shutdowns for maintenance and replacement, resulting in significant losses from unplanned shutdowns.
•Extremely strict environmental and safety controls. High requirements for VOCs fugitive emissions control. Even minor leaks can trigger environmental exceedances and safety hazards, making zero-leakage sealing requirements extremely high.
② Product Compatibility Highlights
• Zero Leakage and High Safety: Utilizing a self-developed magnetic liquid formula adapted to petrochemical conditions, it achieves absolute zero leakage, completely eliminating the risk of fugitive VOC emissions and leaks of flammable and explosive media, fully complying with national petrochemical industry safety and environmental protection standards;
• Long-Term Maintenance-Free Operation: Flexible contact sealing structure with zero friction and wear, allowing for continuous maintenance-free operation. It eliminates the need for frequent shutdowns to replace seals, significantly reducing unplanned downtime losses and improving equipment operating efficiency;
• Strong Corrosion Resistance and Aging Resistance: Customized corrosion-resistant carrier fluid and sealing structure, capable of withstanding common petrochemical corrosive media such as hydrogen sulfide, chloride ions, strong acids and alkalis, and organic solvents for extended periods, solving the pain points of traditional seals being prone to corrosion, swelling, and rapid failure;
• Significant Cost Reduction and Efficiency Improvement: Significantly reduces the manpower and material resources invested in seal procurement and replacement, and equipment maintenance. Simultaneously, it eliminates material losses and equipment damage caused by media leaks. Long-term operation can reduce seal-related comprehensive costs by over 35% for enterprises.;
• Full-scenario customization: It can customize the sealing size, magnetic liquid formula and sealing structure according to different working conditions and equipment specifications (including large-diameter rotating shafts and large reactors) of petrochemical enterprises, and adapt to the full-scenario application from laboratory pilot plants to million-ton-level large-scale integrated refining and chemical plants.
 English
 français
 Español
 العربية
 русский